b-science.net
FAQ Use Cases Blog About Us Register Log In


2026-09-15
Patent Analysis Switch to Visual Summary

Triweekly Patent Update – Free Version

Lithium-ion batteries – electrolytes – all-solid & solid-liquid

CONTEMPORARY AMPEREX TECHNOLOGY CO LTD [CN] / CN 122619951 A

SOLID-STATE BATTERIES AND ELECTRICAL DEVICES

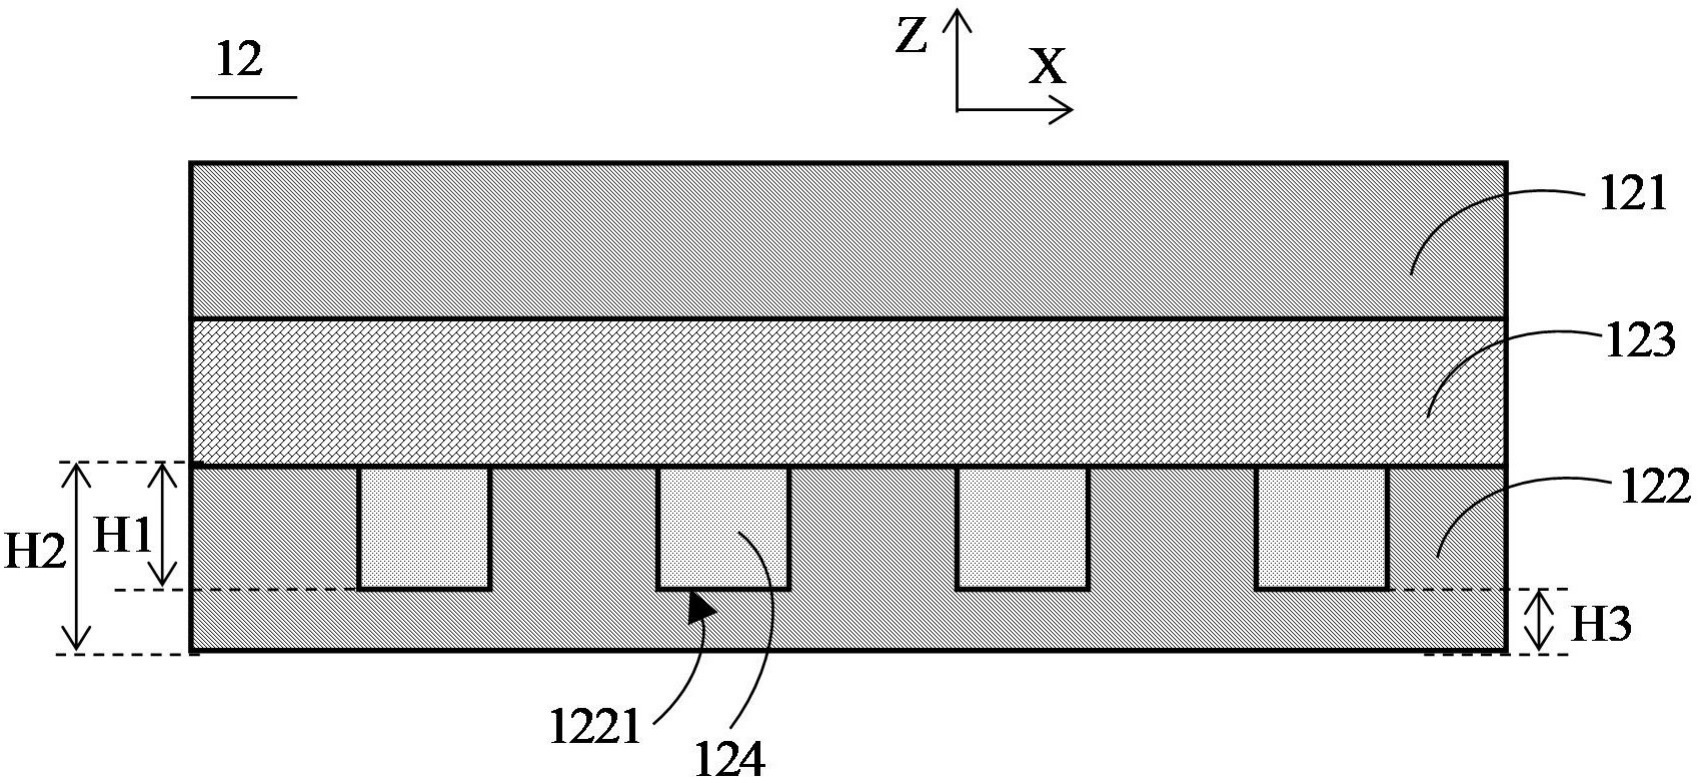
A solid-state cell design places blind holes in the surface of the negative current collector that faces the solid electrolyte layer, so that lithium deposits inside the holes on charge rather than across the collector surface, confining the associated volume expansion below the interface plane.

The holes do not penetrate the collector. The aperture D is 0.01–1 μm and the depth H1 1–10 μm, with D/H1 held at 0.01–0.1. For a collector thickness of 8–50 μm, the holes take up 20–95% of that thickness, leaving an unperforated base of 0.5–8 μm beneath each hole. Polygonal openings have a side length of 0.05–1 μm, and adjacent regular hexagonal openings share a hole wall, giving a honeycomb surface whose walls support one another. The openings cover 5–95% of the surface. The collector is a copper, nickel, titanium or silver foil, or a polymer base layer carrying a metal coating, in which the hole either stops inside the metal or passes through into the polymer. Patterning is by photolithography or by ion or acid etching.

No negative electrode active layer is provided. On charge, lithium plates onto the bottom and walls of each hole to form the lithium-containing metal, which is consumed on discharge, giving an anode-free cell. Both opposing collector surfaces may be patterned. No electrochemical cycling, capacity or interfacial resistance data was identified.

121: positive electrode layer
122: negative current collector (Cu, Ni, Ti or Ag, or a metal-coated polymer film)
123: solid electrolyte layer
124: lithium-containing metal
1221: blind hole
H1: blind hole depth
H2: negative current collector thickness
H3: collector thickness beneath the hole bottom

Figure: Schematic cross-section of the cell, showing the blind holes in the surface of the negative current collector facing the solid electrolyte layer.
CONTEMPORARY AMPEREX TECHNOLOGY CO LTD [CN] / Patent Image
Takeaway: Confining lithium deposition inside recesses in the collector addresses interfacial contact loss geometrically rather than through electrolyte or cathode chemistry. The composite form carries the commercial argument: patterning a thin metal coating on a polymer carrier takes copper out of the bill of materials, a saving that holds at any production volume, while the patterning itself is a process cost that falls as throughput rises. Whether holes of this diameter and depth ratio can be formed at web speed remains the open question.

Lithium-ion batteries – negative electrode (excluding Li metal electrodes)

CABOT CORP [US] / CN 122603411 A

SILICON-CARBON COMPOSITES FOR LITHIUM-ION BATTERY ANODES

A porous carbon black support (LITX HP, Cabot Corporation) served as the scaffold for silicon deposition. The support exhibits an OAN (oil absorption number) of 231.7 ml/100 g carbon, a BET specific surface area of 89.1 m2/g, and an OAN : BET ratio of 2.60, the OAN approximating the void volume available within the carbon black agglomerates.

A thin layer of the carbon black was placed on a quartz tray in a static-bed chemical vapor deposition (CVD) reactor. The reactor was evacuated, purged with argon, and heated to 500°C. Silane (SiH4) was then flowed at 25 sccm for 40 min at 1.3 kPa to deposit silicon inside the pores of the support.

The resulting silicon-carbon composite exhibits a silicon content of 40.6 mass% (thermogravimetric analysis, TGA), equivalent to 64.7 g silicon per 100 g carbon black and below the 0.75 × OAN loading limit of 173.8 g, and a BET specific surface area of 62.0 m2/g as compared to 89.1 m2/g for the silicon-free support. Composites additionally overcoated with carbon (ethylene, 750–1,000°C, 60 kPa, 10 min) were prepared but not evaluated electrochemically.

In half-cells, electrodes of 43.9 mass% composite, 43.9 mass% graphite, 12 mass% lithiated polyacrylic acid (LiPAA), and 0.1 mass% single-walled carbon nanotubes (SWCNT) exhibit an initial capacity of 698 mAh/g, a first cycle efficiency of 78%, and a capacity retention of 66% after 50 cycles (C/20 and C/10 formation, then C/3), as compared to 238 mAh/g, 46%, and 57% for electrodes in which the composite is replaced by silicon-free carbon black.

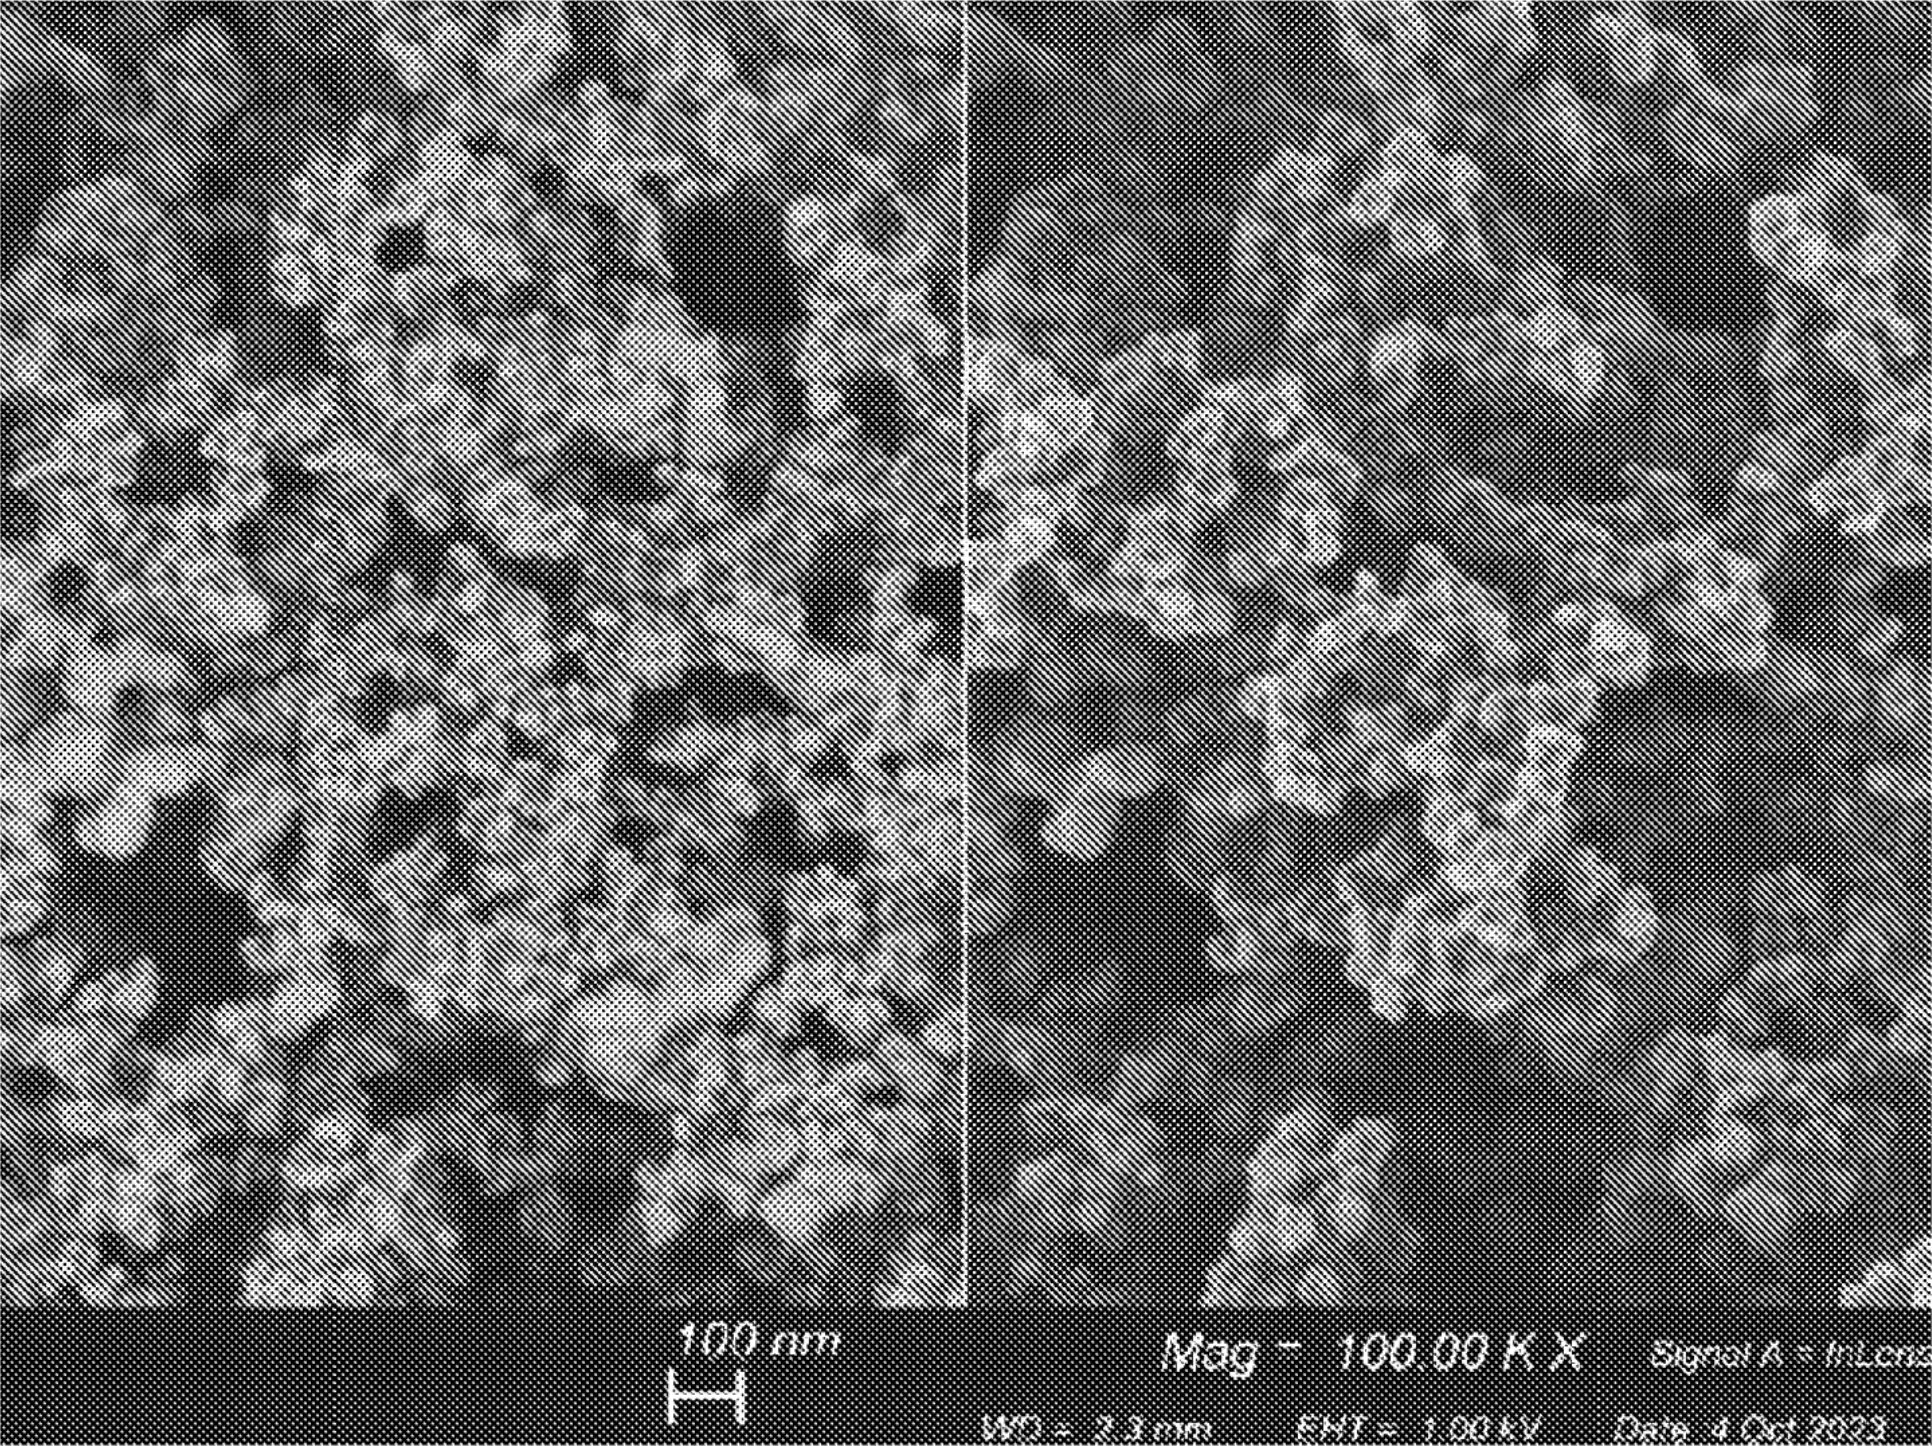
Figure: Scanning electron micrographs of the silicon-carbon composite (backscattered electron signal left, in-lens secondary electron signal right), showing silicon nanoparticles of ≈10 nm carried on the carbon black aggregates and the pore space remaining between them (scale bar: 100 nm).

CABOT CORP [US] / Patent Image
Takeaway: Selecting a carbon black by its OAN : BET ratio – void volume matched to the silicon it must accommodate – defines a scaffold for monosilane deposition, usable alone or within a wider carbon blend, with or without a carbon shell. The same balance could suit the core of core-shell particles: a low external surface area limits solid electrolyte interphase (SEI) formation in liquid carbonate electrolytes, whereas solid-liquid and all-solid electrolytes tolerate higher BET surface areas. In each case the internal void volume is what could suppress particle cracking and electrode height expansion upon cycling.

Lithium-ion batteries – positive electrode

LG ENERGY SOLUTION LTD [KR] / KR 102998175 B1

POSITIVE ELETRODE AND LITHIUM SECONDARY BATTERY INCLUDING THE SAME

Nickel, cobalt, and manganese chlorides (Ni : Co : Mn = 6 : 1 : 3) were dissolved in hydrochloric acid and converted by spray pyrolysis (640°C), jet-milled, washed in distilled water (25°C, 400 rpm, 6 h), and dried (300°C, 1.5 h) to yield the oxide precursor [Ni0.6Co0.1Mn0.3]O2 (BET surface area 7 m2/g), which was mixed with Li2CO3 (Li : (Ni + Co + Mn) = 1.05 : 1) and sintered (960°C, 20 h).

The resulting particles are built from 30 or fewer sub-particle units (nodules), between single-crystal and polycrystalline morphology. EBSD analysis of ion-milled electrode cross sections shows twin boundaries – interfaces between crystallographically symmetric sub-grains – subdividing the nodules, giving a twin density (area-weighted mean crystallite count per nodule, for nodules of ≥1.5 μm equivalent circle diameter) of 2.72. The patent identifies these twin boundaries as additional Li-ion transport paths.

In coin half-cells (0.1 C charge to SOC 20 at 25°C, 2 C discharge for 18 s at −10°C), the material exhibits a low-temperature resistance of 74.4 Ω, as compared to 102.0 Ω for single-particle material made from a co-precipitated hydroxide precursor (twin density 1.10), and to 99.5 Ω for material whose spray-pyrolyzed precursor was not washed (twin density 1.33).

Takeaway: Deliberately introducing twin boundaries into the nodules of single-particle NMC, via a washed precursor from spray pyrolysis rather than co-precipitation, provides additional Li-ion transport paths and lowers low-temperature resistance. The chloride-based route could shorten precursor production by replacing multi-hour co-precipitation with a single thermal step, but the patent does not address chloride off-gas handling (primarily HCl, with Cl2 possible under oxidizing conditions) or reactor corrosion at production scale.

Fuel cells (PEMFC / SOFC / PAFC / AEMFC) – electrochemically active materials

TORAY INDUSTRIES [JP] / WO 2026164032 A1

POLYMER ELECTROLYTE MEMBRANE FOR FUEL CELL, METHOD FOR MANUFACTURING SAME, REINFORCING MATERIAL, CATALYST LAYER-EQUIPPED ELECTROLYTE MEMBRANE, MEMBRANE ELECTRODE ASSEMBLY, FUEL CELL, AND MOVING BODY

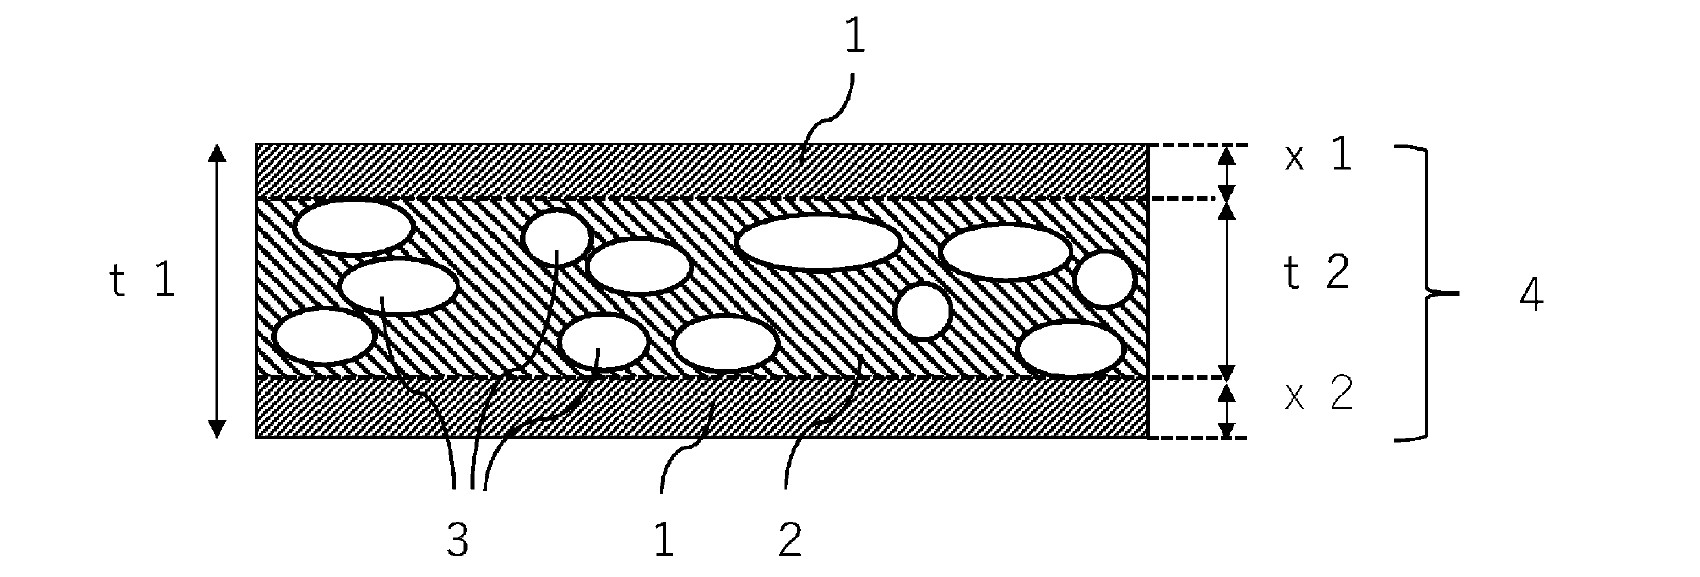
A reinforced polymer electrolyte membrane for PEMFC (proton exchange membrane fuel cell) was developed in which a polyphenylene sulfide (PPS) wet-laid nonwoven sits in the center of a perfluorosulfonic acid (NAFION) membrane, leaving reinforcement-free electrolyte layers at both surfaces (Figure). Thinning the membrane lowers resistance but costs mechanical strength, addressed here through where the reinforcement sits rather than how strong it is.

In Example 8 the reinforcement is a wet-laid nonwoven of drawn PPS skeleton fibers (1.5 μm diameter, 2.0 mm length) and undrawn PPS binder fibers (1.3 μm, 1.0 mm) in a 91 : 9 mass ratio. The sheet was thermally calendered (iron roll 200°C, 490 N/cm, 3 m/min) and UV-irradiated (185 and 254 nm, 10 min), giving a web 4.5 μm thick at 60% porosity. NAFION dispersion was coated onto both faces, dried at 60°C and annealed at 120°C (30 min).

The finished membrane is 8.4 μm thick, of which 5.5 μm contains the reinforcement and 1.5 μm on each face is electrolyte only. It reaches a tensile strength of ≥40 MPa, shows no wrinkling, tearing or pinhole formation after 100 cycles of 80°C water immersion and 100°C drying, and holds its resistance to less than 1.5 times that of an unreinforced NAFION membrane of the same thickness (two-terminal AC impedance, 25°C and 50% RH). Comparative membranes whose reinforcement occupies 48–49% or 89% of the thickness fail the same cycling test. No polarization-curve fuel cell performance data is disclosed.

1: Layer containing no reinforcing material (polymer electrolyte only)
2: Layer containing the reinforcing material
3: Reinforcing fiber cross-section
4: Polymer electrolyte membrane
t1: Polymer electrolyte membrane thickness
t2: Thickness of the layer containing the reinforcing material
x1, x2: Thicknesses of the reinforcement-free layers at either surface

Figure: Cross-section of the polymer electrolyte membrane, showing the layer containing the reinforcing material and the reinforcement-free layers at either surface.

TORAY INDUSTRIES [JP] / Patent Image
Takeaway: The lifetime of an ultrathin membrane is governed less by the strength of its reinforcement than by how deep that reinforcement sits. Holding the nonwoven clear of both faces leaves smooth electrolyte skins for electrode contact and avoids the local stress concentrations that seed wrinkles and pinholes, while a reinforcing band too thin to restrain swelling forfeits the benefit. Managing that placement could make sub-10 μm membranes practical for the high-power stacks targeted at trucks, ships and aircraft.

Other Categories (Excel lists are included for paid users)

  • Lithium metal batteries (excluding Li-S, Li-Air): Excel list
  • Lithium-air batteries: Excel list
  • Lithium-ion batteries – electrolytes – liquid: Excel list
  • Lithium-ion batteries – separators: Excel list
  • Lithium-sulfur batteries: Excel list
  • Na-ion batteries: Excel list